If you’ve ever worked in plastics manufacturing, you know how tiny missteps with material feed can blow up a whole run. A 0.5% overfeed on PVC granules might make the final product brittle; a 0.3% underfeed on recycled polypropylene can slow down molding lines and waste hours of setup time. That’s why our team gets so many calls from plant managers panicking about feeding inconsistencies—they think it’s just a “calibration thing” until a full batch gets rejected or their line drops 20% in efficiency. Today I’m breaking down exactly how plastic feeding equipment pulls off feeding precision (and why it matters way more than you might think), straight from the people who design and tweak these machines every single day. Plastic Feeding Equipment
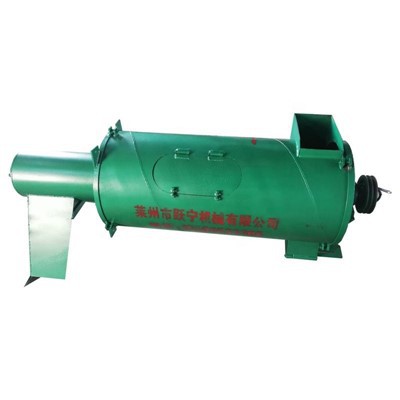
First, let’s clear up a common myth: feeding precision isn’t just “setting a number on a screen.” It’s a combination of hardware built to handle specific plastic materials and software that adapts to the weird quirks of what you’re actually feeding. Plastics aren’t uniform, right? Even resin pellets from the same batch can have minor density differences, recycled material might have tiny clumps, and hygroscopic plastics soak up moisture that makes them clump or flow unevenly. So generic feeders—like basic screw feeders from the 90s—just can’t keep up. The precision control methods we build now start with material-specific hardware tuning. For example, for free-flowing, consistent virgin PP pellets, we use a close-twin single-screw feeder with a tight pitch on the screw flights—this controls the exact volume of material that moves per rotation, with almost no spillover or gaps between granules. But for crumbly recycled PE or fiber-filled plastics that tend to arch in hoppers, we add a vibratory trigger at the hopper base. That vibrates just enough to break up arching without shaking the whole machine, so every pellet moves smoothly into the feed mechanism, no more sudden surges when an arch collapses.
Next, the big one: closed-loop mass flow control. A lot of cheaper feeders use volume-based control—they tell the screw to spin X times per minute, and assume that equals X grams of material. But that ignores density changes! If your resin gets a little more humid overnight, its density goes up, so the same screw rotation dumps more material than it did yesterday, throwing off the whole batch. Our precision feeders run on mass-based closed loops, which means there’s a load cell mounted under the hopper that’s weighing material every 100 milliseconds. Let me explain that simply: the feeder’s controller compares the actual mass coming out of the feed throat to the target mass you input (say, 50 kg per hour), and adjusts the screw speed or vibratory amplitude in real time to close the gap. If a moisture-heavy batch makes the mass jump 0.2% above target, it slows the screw a hair. If there’s a temporary dip from a light hopper load, it speeds up just enough to get back on track. No more waiting for a 15-minute batch test to find out you were off—this adjusts mid-feed, so every minute of production stays consistent. I remember a plant in Ohio that switched from an old volume feeder to our closed-loop model and cut their material waste from 3.2% to 0.8% in the first month alone. That’s thousands of dollars saved on scrap, right there.
Wait, there’s a trick even we don’t advertise as much to new customers: material-specific calibration presets. You can’t use the same calibration for a 3mm HDPE pellet and a 0.5mm micro-granule used in 3D printing filament. Our engineers program presets for every common plastic type, but we also build in a “quick calibrate” feature for custom blends. If a customer is mixing 70% recycled PET and 30% virgin PLA, they don’t have to fumble with manual settings—they can just select their blend, run a 2-minute calibration test where the feeder dumps 1 kg of the blend, and the system learns exactly how that specific mix flows, compacts, and moves through the screw. We even built a little smart tweak for blends that separate: the feeder will alternate short bursts from two separate feed hoppers (one for each resin) instead of dumping both at once, so light micro-resin doesn’t float to the top of the blend. That’s a big one for medical plastics, where even tiny uneven blends can get a part rejected by the FDA.
Now, what about edge cases? We get calls from customers feeding tiny additives—like color masterbatch, which makes up only 0.1% of the total material. A standard feeder can’t handle that, because even a 1% error in the masterbatch feed would make 10% of the product the wrong color. So for micro-additive precision, we use twin-screw micro-feeders, where one screw handles the main resin and a tiny, high-resolution screw handles the additive. The load cell for the micro-additive hopper is super sensitive— it can pick up a 0.1 gram difference in a 100 gram per hour feed. We also use a special anti-backlash gear on the micro-screw, so it doesn’t slip mid-rotation, which is a common issue with cheap gear systems. A customer in Mexico that makes children’s toy plastics used to have a 8% color reject rate because their old additive feeder was inconsistent; switching to our micro-precision unit dropped color rejects to 0.2%. That’s not just efficiency— that’s keeping production on schedule instead of reworking every batch.
A lot of people ask us: can this handle fluctuating line speeds? The answer is yes, and that’s where our feeder’s sync feature comes in. Most feeders just run on their own schedule, but our precision feeders integrate with the molding or extrusion line’s PLC (programmable logic controller) so they feed exactly what the line needs, even if the line speeds up or slows down. If an injection molding line speeds up from 10 cycles per minute to 12, the feeder automatically increases the mass feed rate to match— no overfeeding during fast cycles, no underfeeding when the line slows for tool changes. We’ve had customers use this to reduce line startup waste by 70% — when you start a line, the feeder doesn’t dump a bunch of extra material just to “catch up,” it adjusts smoothly until it’s at the right rate.
Now, let’s talk about common mistakes people make when trying to get precision feeding: cutting corners on maintenance. A feeder is only as precise as its components— if the load cell is covered in dust from plastic resin, it gives bad readings. If the screw flights have a build-up of plastic over time, they don’t move material evenly. We always tell customers to do a monthly quick check: wipe down the load cell, inspect the screw for residue, and run a 1-minute calibration test. We also offer a remote diagnostic tool, so if a customer’s precision drops slightly, our engineers can log into the feeder’s system, check the load cell readings, and adjust a setting without needing to send a technician on-site. That’s saved customers days of downtime, especially for plants that run 24/7.

At the end of the day, feeding precision isn’t a fancy buzzword—it’s the difference between a batch that ships on time and one that’s a total loss, between keeping waste low and blowing budget on scrap. We don’t just sell feeders; we build systems that adapt to what you’re making, because every plastic job is a little different. If you’re dealing with feeding inconsistencies, waste, or product rejects that you can’t figure out, reach out to us to chat. We’ll walk through your process, point out small tweaks you might not have tried, or help you upgrade to a precision feeder that fits your exact needs. No sales pitch, just straight talk about solving your feeding problems.
Plastic Cleaning Equipment References
- Rosato, D. V., & Rosato, M. G. (2012). Extrusion Technology for Plastics. Hanser Publications.
- Plastics Industry Association. (2021). Precision Feeding in Plastics Manufacturing: Best Practices. National Association of Manufacturers.
- Zhang, L., et al. (2020). Closed-Loop Mass Flow Control for Micro-Feeding of Polymer Additives. Journal of Manufacturing Science and Engineering.
- European Machinery Manufacturers Association (EUROMAP). (2019). Standard for Plastic Feeder Precision and Integration.
Laizhou Yuening Machinery Co., Ltd.
As one of the most reliable plastic feeding equipment manufacturers in China, we warmly welcome you to buy cheap plastic feeding equipment made in China here from our factory. All customized machines are with high quality and low price. For pricelist, contact us now.
Address: Yuanjia Village, Luwang, Shahe Town, Laizhou City, Yantai City, Shandong Province
E-mail: yueningjixie@163.com
WebSite: https://www.ynplasticmachinery.com/
