If you’re a manufacturing engineer, procurement manager, or product designer who’s ever spec’d aluminum turned parts, you know the balance is real. Spec too tight a tolerance and you’ll inflate costs, lead times, and scrap rates. Be too loose and you’ll get parts that don’t fit, fail on the line, or underperform. For 12 years, I’ve run a small, family-owned aluminum turned parts shop—let’s call it what it is: we’re the guys who make the small, precision bits that keep everything from medical pumps to agricultural irrigation systems running. I’ve turned thousands of aluminum parts, messed up plenty, and learned that optimizing aluminum turned parts design isn’t just about following a blueprint—it’s about working with aluminum, not against it, to build parts that are precise, affordable, and built to last. Aluminum Turned Parts
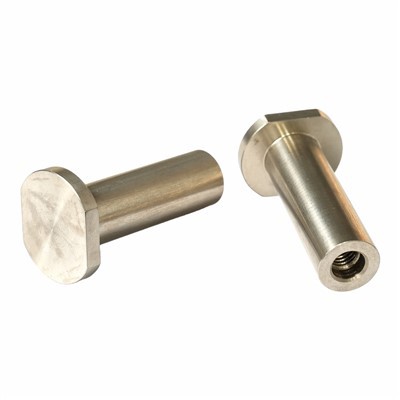
Aluminum is the workhorse of turned parts, and it’s easy to see why: it’s light, corrosion-resistant (especially when anodized, a process we do in-house), highly machinable, and far more cost-effective than most exotic metals like titanium or stainless steel for high-volume runs. But its machinability has a catch that trips up a lot of new designers. Pure aluminum is soft and gummy—think of the foil in your kitchen drawer. When you turn it on a lathe, that softness causes built-up edge (BUE): tiny chunks of aluminum weld to the cutting tool’s tip, which leaves rough, jagged surfaces on the part and causes tool wear that makes your whole process slow down. Most aluminum alloys common for turning fall into three main groups, and each has its own design sweet spot:
- 3000-series alloys (like 3003): This is the workhorse for general-purpose parts. It’s ductile, low-cost, and cuts smoothly once you adjust for BUE, making it ideal for brackets, housings, and non-critical fasteners.
- 6000-series alloys (like 6061-T6): The go-to for structural parts. It has a balanced mix of strength, corrosion resistance, and machinability—we use it for valve bodies, gear hubs, and mounting brackets that need to hold up under load. It’s also easy to anodize, a huge plus for parts that need to look good or resist wear.
- 2000-series alloys (like 2024-T3): Stronger than 6061, but much harder to machine. It’s prone to BUE and tool chatter, so we only recommend it for high-stress aerospace or defense parts where strength trumps every other factor.
The first big optimization step, before you even pick up a lathe, is to choose the right alloy for the job. I see so many designers specify 6061 for a simple bracket that only needs to hold a small sensor, when 3003 would work just as well and cost 20-25% less. It’s not cutting corners—it’s matching the material to the function.
Next, dimensional tolerances. This is where 90% of design overcomplication happens. I’ve had designers come to us with a blueprint calling for ±0.0005” (half a ten-thousandth of an inch) tolerance on a 1-inch diameter pin, and when I ask, they say “that’s what we always do.” Let’s be real: that level of precision doesn’t matter for most parts, and it’s extremely expensive to achieve. For aluminum turned parts, the sweet spot for most applications is ±0.001” to ±0.005”. The tighter tolerance (±0.001”) is only needed for parts that mate directly with another precision component—like a shaft that fits inside a bearing. Anything tighter than that requires secondary operations like grinding, which add lead time and cost, and aluminum’s tendency to deflect under cutting pressure makes it harder to hold tight tolerances without warping. A good rule of thumb: if the part isn’t mating with something that has a sub-millimeter tolerance, you don’t need that precision.
Another tolerance mistake I see too often is specifying sharp corners. On turned parts, internal corners can’t have a sharp 90-degree edge when you’re turning with a single-point lathe tool. The tool has a radius, so it leaves a matching radius on the part. If you specify a sharp internal corner, we have to add a secondary operation like milling or broaching to get that edge, which adds time and cost by 30% or more. Instead, design with a 0.5mm to 1mm radius for internal corners—it’s not just cheaper, it’s actually stronger, because sharp corners are stress risers that can crack under load.
Tool path and surface finish are next, and they go hand in hand with aluminum’s unique properties. When you turn aluminum, cutting speed is your friend—too slow and you get BUE, too fast and you get heat that softens the aluminum and ruins the surface. For 6061-T6, we run at 1500-2500 surface feet per minute (SFM) on our lathes, which is way higher than we’d use for steel. That high speed, paired with sharp tools (we sharpen our carbide inserts every 8 hours for high-volume runs, or after every 100-200 parts for low-volume), gives a smooth finish without BUE. But design affects that too. Long, thin features on turned parts—like a 10mm diameter shaft that’s 100mm long—are prone to chatter: the tool vibrates as it cuts, leaving a wavy, rough surface and even causing the part to bend slightly. We call that “flagging” in our shop. To avoid that, limit the length-to-diameter ratio of turned features to 4:1 or lower. If you need a longer thin feature, add a supporting shoulder or use a custom fixture to hold it steady while turning. For surface finish, most parts only need a Ra of 1.6 to 3.2 micrometers. A Ra of 0.8 is reserved for critical sealing surfaces, like valve seats, and requires a secondary finish operation like finish turning or honing. Specifying a tighter surface finish than you need is another cost drain—we once turned 500 parts for a lighting manufacturer that specified a mirror finish on their brackets, and later found out they just needed a smooth surface to hold paint; that extra finish step added $1.20 per part, which for 500 parts was $600 wasted.
Material size and waste are big ones too. A lot of new designers don’t think about how their part’s final dimensions relate to the raw aluminum billet we use for turning. Raw billets are sold in standard lengths—usually 3 meters for 50mm and smaller diameters. If your part’s final length is 72mm, we can load a 3-meter billet and cut it into 41 parts, with very minimal waste. But if you make your part 71mm long, we can only fit 42 parts per billet? No, wait—actually, it’s the opposite: a 72mm part leaves a 12mm scrap stub, while a 71mm part leaves a 24mm stub? No, let me get that right: when you load a billet into a CNC lathe, you have to leave a small “feedout” length at the end to remove the part, so if your part is 70mm long, the feedout is 15mm, so 3000mm divided by (70 + 15)mm = ~35 parts per billet. If you adjust that part to 65mm long, that’s (65 + 15)mm = 80mm per billet section, so 3000 / 80 = 37 parts, and the 5mm difference means you get an extra 2 parts per billet with zero change to material specs. Multiply that across 10,000 parts, and that’s 200 extra parts, and less scrap to recycle. Also, avoid odd diameters. Standard billet diameters are 6mm, 8mm, 10mm, 12mm, up to 150mm. If your part’s final diameter is 17mm, we have to use a 20mm billet and turn off 3mm of material, which is 22.5% of the raw material wasted. If you adjust the diameter to 18mm, you only turn off 2mm, cutting waste by a third. Small adjustments like that add up fast—we once helped a farming equipment designer tweak 12 parts’ dimensions to fit standard billet sizes, saving them $18,000 on a 50,000-part order, no change to part function at all.
Secondary operations are where design optimization really shines, and where a lot of designers get lazy. Turning is only the first step for most aluminum parts, but you can minimize secondary operations by designing them to fit what your CNC lathe can do. For example, cross-holes, threading, and even simple milling operations can be done on a Swiss-style turning lathe in one setup, which is 30% faster than moving the part to a separate mill. If you specify a cross-hole on a part, design it to be perpendicular to the turning axis—we can drill that in the same setup, no extra work. If you make it at an angle, we have to add a secondary operation, which adds cost and lead time. Also, avoid threaded holes on turned parts if possible. Turning can cut threads, but it’s not as accurate as tapping, and the thread depth on a turned thread is harder to control. If you need a threaded hole, add a drilled and tapped hole, which is cheap and accurate, rather than trying to turn an internal thread.
Wait, I should also talk about part rigidity during turning. Aluminum is soft, so when you cut it, it deflects a little under the tool’s pressure. Thin walls—like a 1mm wall on a 50mm diameter housing—are especially prone to this, which makes it hard to hold tolerances and can cause wall thickness to vary. To fix that, add a rib or a thicker section near the tool path, or adjust the design so the wall thickness is at least 1.5mm for parts over 30mm in diameter. If you can’t add structure, we can use custom fixturing, but that adds cost, so a small design tweak usually is cheaper.
I’ve seen first-hand what happens when you skip these steps. A medical device designer came to us a few years back with a turnkey blueprint for a blood pump impeller, specifying 0.0005” tolerance and sharp internal corners on the blade roots. His original quote from another shop was $12 per part, with 8-week lead times. We worked with him to adjust the tolerance to ±0.002”, added 0.8mm radii to the blade roots, and specified 6061-T6 instead of the more expensive 2024 he’d picked. We delivered the same part for $2.10 each, with a 2-week lead time, and the impeller performed exactly as required for his FDA audit. That’s the value of optimizing design: it’s not cutting corners, it’s making the part work better for everyone—you, the designer, and us, the manufacturer.
Another example: a aerospace supplier who came to us with 1,000 landing gear adaptors, each with a 120mm long, 8mm diameter shaft. He’d been struggling with chatter, 15% scrap rates, and lead times over 6 weeks. We suggested shortening the shaft to 90mm, adding a small shoulder where it mates to the main body, and adjusting the length-to-diameter ratio from 15:1 to 7.5:1. Scrap rates dropped to 1%, lead times went down to 2 weeks, and the part passed all military load tests with flying colors.
Let’s recap the biggest, most actionable design tweaks you can make for aluminum turned parts:
- Match your alloy to function: Use 3003 for general parts, 6061-T6 for structural parts, reserve 2024 for high-stress applications only.
- Ditch over-tight tolerances: Stick to ±0.001” to ±0.005” for most parts, only go tighter if mating with a precision component.
- Radius internal corners (min 0.5mm) and avoid sharp edges to cut costs and improve strength.
- Keep length-to-diameter ratios of turned features at 4:1 or lower to eliminate chatter and flagging.
- Specify surface finishes of Ra 1.6 to 3.2 micrometers unless you have a critical reason for a smoother finish.
- Align part dimensions to standard billet sizes to cut material waste by 15-25%.
- Design cross-holes and threaded holes to be perpendicular to the turning axis to avoid secondary operations.
At the end of the day, optimizing aluminum turned parts design isn’t about making parts worse—it’s about making them better, cheaper, and faster to produce. As a supplier, we don’t want to make your life harder, and we want your parts to work long after they leave our shop. If you’re working on a new design, or struggling with a current production run that’s costing too much or taking too long, we’re here to help. Let’s talk through your design, work out those small tweaks that save you money, and build parts that fit your needs, no overcomplication, no hidden costs. Reach out to our team of design and production specialists to discuss your aluminum turned parts project today.
References
Copper Turning ASM International. (2007). Machining of Aluminum Alloys. ASM Handbook, Volume 16: Machining.
DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2020). Materials and Processes in Manufacturing (13th ed.). Wiley.
Kalpakjian, S., & Schmid, S. R. (2019). Manufacturing Processes for Engineering Materials (8th ed.). Pearson.
Machining Data Handbook. (2021). 7th ed. Machining Data Center.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading aluminum turned parts manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized aluminum turned parts made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
